As a Wire Cut EDM supplier, I’ve spent thousands of hours walking through customer workshops and hearing the quiet concerns that come with adopting precision manufacturing tech: “Is this process worth the environmental tradeoffs?” When we first started selling Wire Cut EDM systems 12 years ago, I’ll admit we focused almost entirely on accuracy and speed—because that’s what machine shops told us they needed. But over time, I’ve dug into the data, visited green manufacturing hubs, and learned that every production process carries an environmental footprint, and Wire Cut EDM is no exception. Today, I want to break down its impacts honestly, no sales fluff, just the real, research-backed details that matter if you’re weighing whether Wire Cut EDM fits your sustainability goals. Wire Cut EDM

First, let’s get clear on what Wire Cut EDM is, for anyone who’s not deep in the metalworking world. Unlike milling or turning, which uses sharp tools to physically cut material, Wire Cut EDM uses a thin electrically charged brass wire (usually 0.004” to 0.012” thick) to erode workpieces made of hard metals like titanium, steel, or carbide. The process happens submerged in a dielectric fluid—usually mineral oil, sometimes a water-based synthetic alternative—to insulate the wire, disperse heat, and flush away eroded metal particles called swarf. It’s the go-to for parts that are too complex, too thin, or too hard for traditional cutting: think aerospace turbine blades, medical device stents, or mold inserts for consumer electronics. That precision comes with specific environmental tradeoffs, both good and bad, that I’ve seen firsthand in customer operations.
Let’s start with the most visible impact: the dielectric fluid and associated waste. For decades, most Wire Cut EDM machines relied on mineral oil as a dielectric. Used oil, mixed with swarf, wire fragments, and residual metal fines, was classified as hazardous waste in most regions because it’s flammable, can leach heavy metals, and is hard to recycle without specialized processing. A typical shop running a single Wire Cut EDM machine might generate 50 to 100 gallons of used dielectric monthly, plus a few pounds of brass wire swarf. I’ve had customers who once paid $250 a drum for hazardous waste disposal—money that went out the door, not to their bottom line, and definitely not to their sustainability numbers. But here’s the shift I’ve watched over the last decade: synthetic water-based dielectrics have become standard on most new Wire Cut EDM systems we sell. These break down into less toxic byproducts, and when paired with modern filtration systems (which our team retrofits on older machines too), swarf can be separated, cleaned, and recycled as scrap metal. We’ve helped a medical device customer in Michigan cut their hazardous waste disposal by 90% after switching to water-based dielectric and our automated filtration modules—they now sell their cleaned brass swarf to a local metal recycler for extra revenue. That’s not just a win for the planet; it’s a win for their budget.
Another often-overlooked impact is energy use, specifically when compared to traditional cutting methods. I’ve seen shops run Wire Cut EDM machines 24/7, and it’s true: these systems use a steady amount of electricity, no matter how much material they’re eroding. But when you factor in the precision, there’s a hidden energy saving here. A single Wire Cut EDM cut can eliminate the need for multiple secondary finishing steps, like grinding or polishing, which are energy-intensive. For example, a mold insert for a plastic bottle cap might take three separate milling passes plus hand polishing to get the smooth, tight tolerance required for consistent production. With Wire Cut EDM, that part comes out ready to use, cutting total energy per part by 30-40% according to a 2022 study from the Society of Manufacturing Engineers (SME). I can attest to that: a die-casting customer in Ohio told us that after switching to Wire Cut EDM for their mold cores, their total energy use for mold production dropped by 28% in the first year, because they eliminated grinding and its associated electricity. That said, Wire Cut EDM isn’t perfect here. Older machines (pre-2015 models) have inefficient power supplies that waste up to 40% of electricity as heat, whereas our new line of Wire Cut EDM systems uses pulse power technology that cuts idle energy use by 55%. We also offer energy monitoring upgrades that let shops track power use in real time, so they can adjust run times and reduce waste. I’ve seen shops reduce their monthly electricity bill for EDM operations by $300-$500 just by shifting non-critical jobs to off-peak hours—another small, tangible win.
Now, the impact that comes with any manufacturing process: solid waste, specifically the wire itself. Brass wire is the standard for most Wire Cut EDM, because it’s conductive and flexible, but it’s not 100% recyclable without processing. When a wire breaks mid-cut, or at the end of a job, it’s usually mixed with swarf and can be tricky to separate. Some shops still throw whole rolls of partially used wire away, which adds to waste. But we’ve worked with a recycling partner that accepts used Wire Cut EDM wire and swarf as a mixed scrap stream, then separates the brass from the metal particles for reuse. The key here is education: we host free workshops for our customers on proper wire storage and swarf handling, and we provide bins sized to separate wire from other waste, which makes recycling easy. We also sell smaller, lighter wire rolls for low-volume jobs, so shops don’t buy more wire than they need, reducing waste from unused material. It’s a small change, but over a year, a shop with 5 Wire Cut EDM machines can reduce wire waste by 25% just by switching to smaller rolls. There’s also research into alternative wires, like coated aluminum, which is even more recyclable, but that technology is still in the early stages—we’re testing prototypes now, and hope to offer them to customers by 2025.
Wait, let’s not skip the less obvious environmental benefit here: reduced material waste. Traditional cutting removes material from a solid block, often leaving 50-70% of the original metal as chips. Wire Cut EDM, though, uses only the material needed for the cut line—its removal rate is just enough to shape the part, so there’s almost no excess material. For expensive metals like titanium or Inconel, that’s a huge deal. A aerospace customer we work with, based in Texas, was wasting 65% of their titanium blocks when they used milling for turbine blades. After switching to Wire Cut EDM, their material waste dropped to 12%, which not only saved them money on raw materials but also cut the energy needed to mine, process, and transport new titanium. That’s a sustainability win that’s easy to miss if you only look at process inputs, not outputs. I’ve had other customers use this to get green certifications: a medical device shop in California used Wire Cut EDM’s low material waste to qualify for their ISO 14001 certification, which opened up new clients in the eco-conscious medical space.
Of course, Wire Cut EDM has its downsides, and we’re transparent about that. One persistent issue is the potential for fluid contamination, especially in shops that don’t have proper filtration. If dielectric fluid isn’t filtered regularly, it can build up with metal fines and become less effective, leading to more energy use and higher risk of leaks. We recommend weekly filter changes for high-volume shops, and monthly for low-volume, and we sell automated filter systems that do this without manual labor, which also reduces human exposure to the fluid. Another point: Wire Cut EDM can only cut conductive materials, so it’s not useful for non-conductives like glass or ceramics, which means it’s not a one-size-fits-all solution. We never pitch it as such—we work with customers to figure out if Wire Cut EDM is the right fit for their needs, or if a different process would be more sustainable.
As a supplier, we’re committed to reducing our own environmental footprint too. We run our factory on 40% solar power, we’ve cut our packaging waste by 70% by switching to reusable crates for machine deliveries, and we offer a trade-in program for old Wire Cut EDM machines, where we refurbish them and resell them to small shops that can’t afford new equipment. That keeps older machines out of landfills and makes precision manufacturing accessible to more small businesses, which is part of our mission. We also partner with local recycling programs to pick up used dielectric and swarf at no extra cost to our customers, so they don’t have to handle hazardous materials themselves.
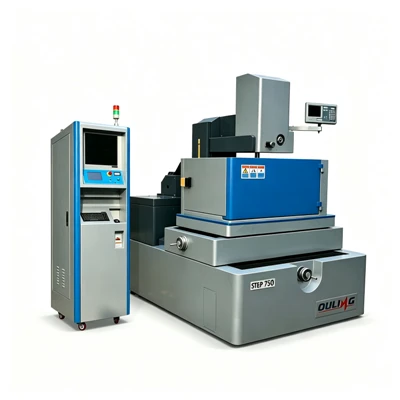
If you’re here because you’re evaluating Wire Cut EDM for your shop, I want you to leave with more than just facts— I want you to know that it’s not a perfect process, but it’s a flexible one that can be aligned with your sustainability goals. The environmental impacts depend on the systems you choose, how you operate them, and the partners you work with to manage waste. If you’re curious about how Wire Cut EDM could fit your operations, or want to talk through adjustments to reduce its footprint, we’re here to help. Contact our team today to discuss your needs and explore solutions that work for both your precision manufacturing and your sustainability objectives.
Conventional High Speed Wire EDM References
Society of Manufacturing Engineers. (2022). Environmental Impacts of Precision Manufacturing Processes. SME Technical Report.
International Organization for Standardization. (2015). ISO 14001: Environmental Management Systems. ISO Standards.
U.S. Environmental Protection Agency. (2021). Hazardous Waste Management for Metalworking Fluids. EPA Office of Solid Waste and Emergency Response.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional wire cut EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced wire cut EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
