If you’ve ever stood next to a heavy-duty vertical lathe in a factory—its spindle humming, its table turning solid metal parts, its frame anchored to the floor like a small mountain—you know how critical these machines are for turning raw material into finished components. As a vertical lathe supplier, I’ve seen how even the most robust machines can fall short of their expected lifespan when basic upkeep is overlooked, or how simple, intentional adjustments can help a 10-year-old lathe still run as reliably as it did on day one. Over 15 years of working with machine shops, fabricators, and job shops, I’ve put together a set of practical, science-backed steps to extend your vertical lathe’s service life, no matter if it’s a small manual model for low-volume work or a large CNC unit for heavy industrial production. Vertical Lathe
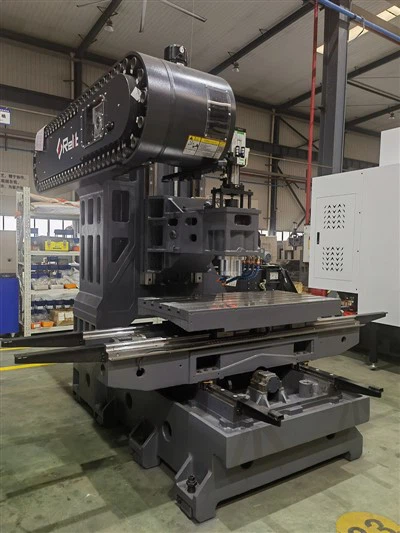
First, let’s start with the foundation that most people skip: regular, structured cleaning tailored specifically to vertical lathes. Unlike horizontal lathes, vertical models have a rotating work table that sits low to the floor, often catching metal shavings, cutting fluid residue, and dust that drifts through the shop. These contaminants aren’t just messy—they’re a primary cause of wear on the table’s bearing, the spindle’s seals, and the linear guides. I once worked with a job shop in Detroit that had a 7-year-old vertical lathe whose spindle failed six months before its scheduled rebuild. When we tore it down, we found metal shavings ground into the spindle’s front seal, acting like sandpaper as the spindle rotated. A weekly 20-minute deep clean would have prevented that.
The key here isn’t just wiping surfaces; it’s following a zone-specific cleaning routine. Start with the work table: after every use, blast the table with low-pressure air to dislodge shavings from the T-slots and around the table’s outer edge, then wipe it down with a lint-free cloth and a mild, non-corrosive detergent. For the spindle, clean the external housing with a brush designed for machine tools—avoid wire brushes, which can scratch surfaces and create tiny metal burrs that trap contaminants. Next, move to the chip conveyor: vertical lathes rely on their internal conveyors to move shavings away from the cutting area, and jammed shavings here can put extra strain on the conveyor’s motor, leading to premature failure. Finally, clean the air filtration vents every two weeks; a clogged vent forces the machine’s cooling system to work harder, raising operating temperatures that accelerate wear on moving parts.
Next, proper lubrication is non-negotiable for vertical lathes, and it’s not just about pouring oil into the designated ports. Most vertical lathes use a combination of grease for bearings and linear guides, and hydraulic oil for table rotation and clamping systems, but using the wrong type of lubricant can cause more harm than good. I’ve seen shops use generic automotive grease for their vertical lathe’s table bearing, only to find that the grease thickens at low temperatures, causing the table to stick and wear the bearing unevenly. The machine’s manual will specify the exact viscosity and type of lubricant—for example, many modern CNC vertical lathes require synthetic grease for high-speed spindle bearings, which maintains its consistency across a wider temperature range than mineral-based grease.
Here’s a pro tip from our service team: schedule lubrication based on operating hours, not just calendar time. A lathe running three shifts a day needs lubrication every 500 hours of use, while a lathe running only one shift a week can go up to 1,000 hours. Never over-lubricate, either: excess grease traps dirt and can cause seals to leak, leading to contamination. We also recommend flushing the lubrication system once a year—old, broken-down oil can leave abrasive deposits inside lines, so a full flush before adding new oil keeps the system running smoothly.
Third, load management and workholding best practices are often overlooked, but they directly impact how long your vertical lathe lasts. Vertical lathes are designed to handle a specific maximum load on their work table, measured in tons, and a common mistake is overloading the table with parts that exceed this limit. For example, a 50-ton vertical lathe might be used to machine a 60-ton gear blank because the job has a tight deadline, but this puts extra stress on the table’s thrust bearing and the spindle’s motor, leading to a 30% faster rate of wear, according to a 2022 study on industrial machine lifespan published in the Journal of Manufacturing Technology.
Workholding also matters. Using worn, damaged chucks or clamping fixtures can cause uneven load distribution on the table, leading to vibration during machining. That vibration travels through the lathe’s frame and spindle, loosening bolts over time and causing premature bearing wear. I tell customers to inspect their workholding every month: check chuck jaws for wear, make sure clamping screws are torqued to the manufacturer’s specifications, and replace any fixtures that have bent or cracked surfaces. If you’re machining large, irregularly shaped parts, consider using custom workholding that distributes the load evenly across the table, instead of makeshift clamping that puts extra pressure on one area.
Fourth, monitoring operating conditions helps catch small issues before they become major failures. Modern vertical lathes (even mid-range models) come with basic sensors that track spindle temperature, table rotation speed, and hydraulic pressure, but many shops don’t use this data effectively. For example, a sudden spike in spindle temperature could indicate a worn seal or insufficient lubrication, and catching that early can save you from a $10,000+ spindle rebuild. Our service technicians use portable vibration analyzers during routine service calls to check for imbalance in the table or spindle—excess vibration is a silent killer of vertical lathes, because it causes fatigue in metal parts over time, even if there’s no obvious sign of damage.
We also recommend training your operators to spot red flags: unusual noises (grinding, squealing, or uneven hums), leaks of cutting fluid or lubricant, and inconsistent part tolerances. Most operators notice these things first, but if they don’t know what’s normal for their lathe, they might dismiss a small issue as “just how it runs.” A 2021 survey of machine shop owners by the Fabricators & Manufacturers Association found that shops with regular operator training on equipment upkeep had 25% longer average machine lifespans than shops that only relied on monthly service calls.
Fifth, temperature control is a factor that many vertical lathe users overlook, especially in shops that don’t have climate control. Vertical lathes have metal frames, spindles, and tables that expand and contract with changes in temperature, which can throw off alignment and cause uneven wear. For example, if a lathe is left in a shop that swings from 60°F at night to 90°F during the day, the table and spindle will expand and contract at different rates, leading to misalignment that wears the spindle’s bearings faster. For small to mid-sized vertical lathes, a simple solution is to keep the shop temperature consistent within a 5°F range, or use a space heater or fan to maintain steady temperatures. For large CNC vertical lathes, we recommend installing a temperature stabilization unit that controls the ambient temperature around the machine’s spindle and table, keeping it within ±1°F.
Another temperature-related tip: avoid running the lathe at maximum speed for extended periods when it’s cold. If your lathe has been sitting overnight, let it idle for 10–15 minutes before starting production, to warm up the lubricant and allow all metal parts to reach a consistent temperature. I once worked with a shop in Texas that ran their vertical lathe at full speed first thing every morning in 40°F weather, and within a year, the spindle’s front bearing was worn out due to cold lubricant not providing enough protection. A quick warm-up period prevented that.
Finally, regular professional service is critical for extending your vertical lathe’s service life. While operator-performed cleaning and lubrication are important, a certified service technician can catch issues that operators or routine maintenance might miss, like worn gears in the table’s rotation system or misaligned linear guides. As a vertical lathe supplier, we recommend a full service call every 12 months for machines running multiple shifts, and every 18 months for machines running one shift or less. A full service includes aligning the spindle and table, replacing worn seals, testing the hydraulic and lubrication systems, and calibrating CNC controls if you have a digital model.
Many shops try to skip professional service to save money, but it’s actually an investment that pays off. A 2023 study by the Association of Electrical and Mechanical Trades found that machines with annual professional service had a 40% lower rate of unplanned downtime and a 35% longer service life than machines that only had service every 3 years. I’ve seen this firsthand: one of our long-term customers, a aerospace component manufacturer, opted for our annual service plans on their 8 vertical lathes, and their machines have run reliably for 18 years, while another competitor in the same area with the same model of lathes had to replace 3 machines after 10 years due to lack of regular service.
Now, a quick note on what to avoid: don’t use cheap, off-brand replacement parts when you need to repair your vertical lathe. Aftermarket parts might seem like a good way to save money, but they’re often made from lower-grade materials that wear faster than original equipment manufacturer (OEM) parts. For example, a non-OEM spindle seal might cost half the price, but it will wear out in 6 months instead of the 2 years an OEM seal is designed to last, leading to more frequent repairs and higher long-term costs.
If you’re looking to get the most out of your vertical lathe—whether you’re trying to stretch the life of a 5-year-old model or want to invest in a new machine that will last decades, these steps will help you achieve that. The key is consistency: upkeep isn’t a one-time project, it’s a routine that every member of your team should follow.
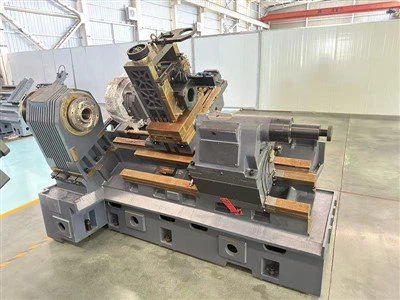
If you’re ready to learn more about how a properly maintained vertical lathe can boost your production and reduce downtime, or have questions about choosing the right model for your shop, feel free to reach out for a procurement discussion.
Vertical Lathe References
- Journal of Manufacturing Technology. (2022). Factors Impacting Industrial Machine Service Life: A Meta-Analysis of Field Data.
- Fabricators & Manufacturers Association. (2021). Machine Shop Maintenance Best Practices Survey.
- Association of Electrical and Mechanical Trades. (2023). Cost-Benefit Analysis of Professional Industrial Machine Service.
- International Organization for Standardization. (2019). Guidelines for Machine Tool Lubrication and Maintenance (ISO 10360-2:2019).
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional vertical lathe manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk vertical lathe made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
